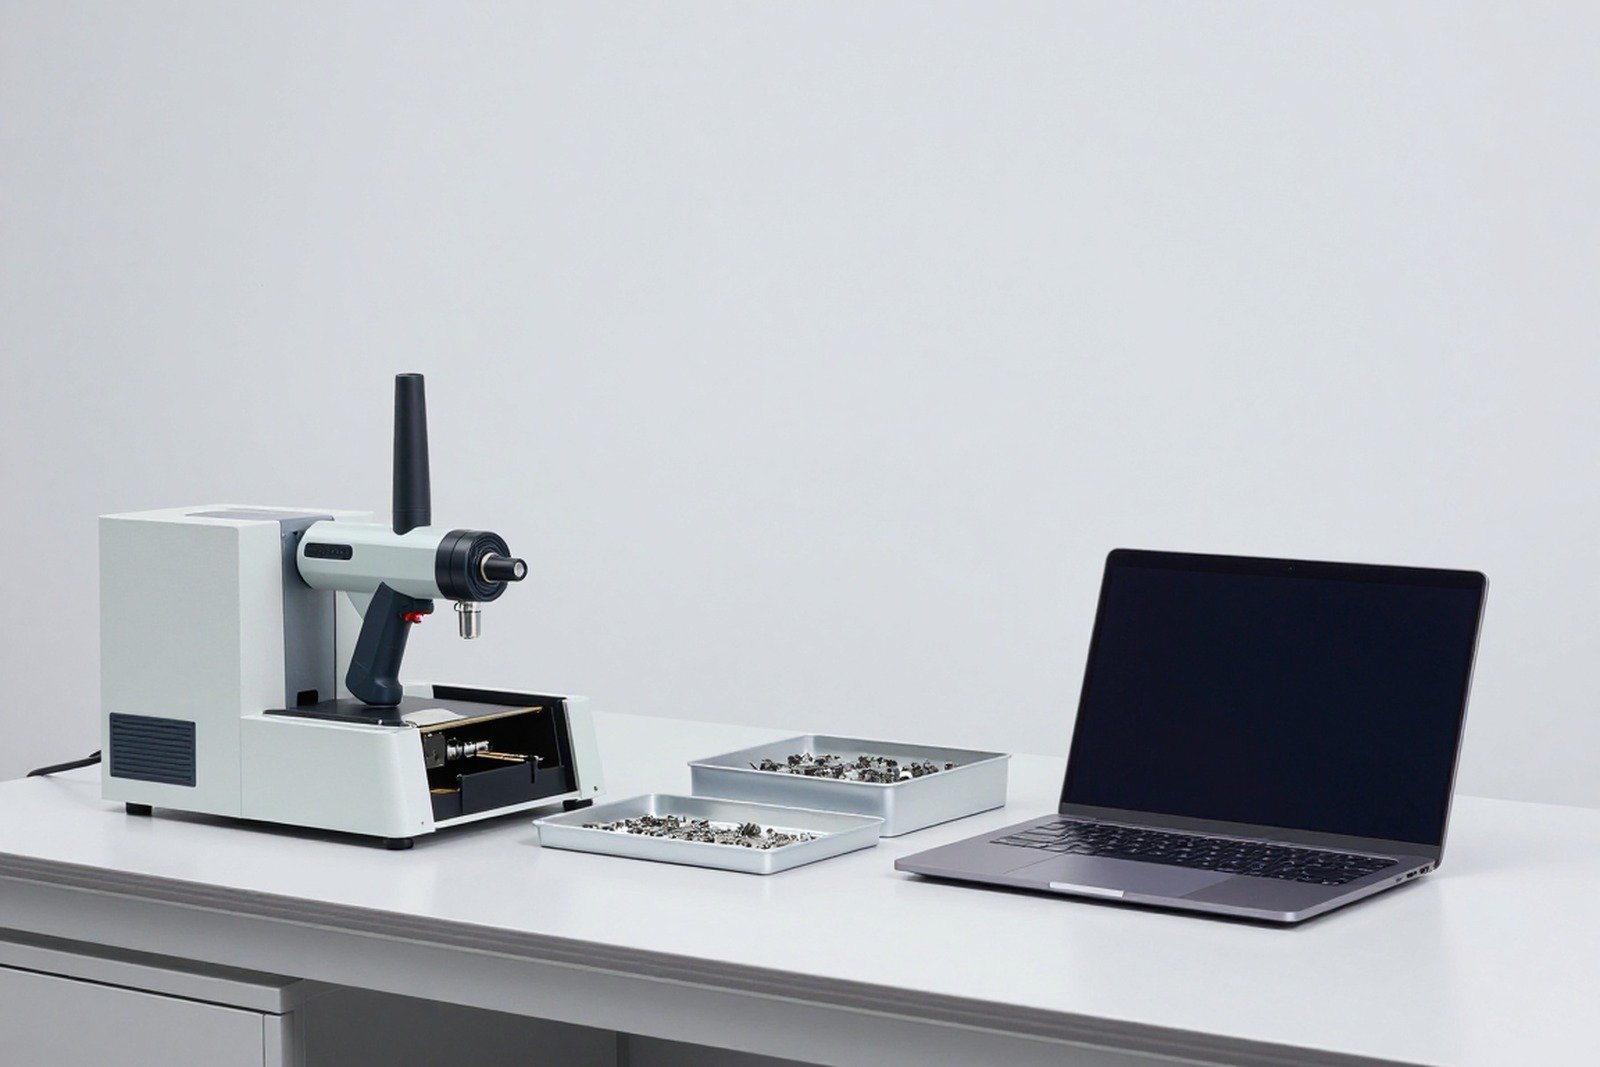
One of the most practical questions when building a RoHS control system is: can XRF be used for everything, or is wet testing required? Short answer: XRF is a very good screening tool, but four technical limitations prevent it from replacing wet testing for concluding conformity.
Correctly understanding the boundary between the two tools helps businesses save significantly: using XRF to localize risks and control each batch, using wet testing for points that really need to be concluded. Conversely, using XRF in the wrong place will create a false sense of security and returned shipments.
1. What can XRF do and what can’t it do?
| Possibility | XRF | Notes |
|---|---|---|
| Measure total elemental content (lead, mercury, cadmium, chromium, bromine) | Yes | Is the main strength of XRF, especially in input screening |
| Distinguish between trivalent chromium and hexavalent chromium | No | XRF only indicates total chromium; Need a separate method to determine chemotherapy |
| Detect PBB, PBDE | Not directly | Only total bromine can be measured, compounds cannot be distinguished |
| Detection of phthalates | No | It is an organic compound, not within the measurement range of XRF |
| Measure cadmium at very low limit levels | Limitations | The detection limits of many handheld devices are not enough to draw close conclusions |
| Measure powder materials, small samples, multi-layer paints | Limitations | Proper sample preparation is necessary, otherwise the results will be strongly influenced by the sample matrix |
In other words: XRF answers the question “does this material present a risk”, not “does this material meet the RoHS limit” in all cases.
2. Four cases require wet testing
- XRF results are near the limit. When measurements are close to the limit, measurement errors can reverse the conclusion — requiring more precise analysis methods.
- Need to conclude about hexavalent chromium. XRF reports total chromium, does not show valence; this is the most common reason why a material that “passes XRF” still requires further testing.
- Need to conclude about PBB, PBDE and phthalate. These are organic compounds, so chromatography combined with mass spectrometry must be used.
- Need conclusion for legal documents. When customers or supervisory authorities require evidence, standard method test reports have a higher value than screening results.
3. XRF screening is still very valuable: use it correctly
The greatest value of XRF does not lie in replacing wet testing, but in reducing the number of wet testing points and detecting abnormal materials early:
- Input Control: Screen each batch of high-risk materials such as welds, plating, alloys, and flame retardant plastics.
- Compare with standard sample: Compare the new batch results with the confirmed batch to detect any unusual differences.
- Zoning in products: Determine which parts need wet testing, instead of testing the entire product.
- Quick check when changing suppliers: a few minutes measurement can prevent a defective batch.
4. Decision table: XRF or wet test?
| Situation | The right tool | Reason |
|---|---|---|
| Quickly check imported batches against standard samples | XRF | Fast, non-destructive, enough to detect abnormalities |
| Confirm material meets limit for filing | Try wet | Need standard methods and quantitative results |
| Materials with chromium in the plating or passivation layer | Wet test (chemical determination) | XRF does not distinguish between chemotherapy |
| The plastic contains brominated flame retardants | Wet test (mass spectrometry) | It is necessary to distinguish PBB/PBDE from other flame retardants |
| Soft plastic, cable cover, gasket | Wet test (phthalate) | XRF does not measure organic compounds |
| Powdered materials, very small samples or multiple layers | Wet test or special sample preparation | The sample matrix strongly influences XRF |
| Screening results are close to the limit | Try wet | More precision is needed to conclude |
5. Develop a three-layer control strategy
An effective implementation is to divide materials by risk level and associate each level with an inspection frequency:
| Material class | Risk level | How to control |
|---|---|---|
| Solder joints, plating, brass alloy, contacts | High | Screen each batch, wet test periodically |
| Soft plastic, cable cover, gasket, handle | High | Periodic screening, periodic phthalate testing |
| Recycled plastic, unstable source materials | Very high | Control each batch of raw materials |
| Common unplated metals, glass, ceramic | Low | Material declaration, probability check |
| Auxiliary materials: glue, ink, stamps, packaging | Average | Declare and test when changing suppliers |
6. Frequently asked questions
When XRF reports “Pb” exceeds the limit, is it definitely a defective product?
Not sure yet. Results may be affected by sample matrix, coating, or measurement location. It is necessary to re-measure at another point, on a properly prepared sample, and for official records, a quantitative analysis method is needed.
XRF reports that chromium exceeds the limit, is it hexavalent chromium?
Need to determine separately by appropriate method. Many plating and passivation layers use trivalent chromium, which is not subject to that restriction. This is the most common misunderstanding when working with XRF results.
Can XRF be used to test for phthalates in cables?
No. XRF does not measure organic compounds. Mass spectrometry is needed for the phthalate group.
Is there any equipment that can screen bromine to deduce PBDEs?
XRF measures total bromine, which is useful but not conclusive. Plastics with brominated flame retardants that are not on the restricted list may still give high bromine results; On the contrary, plastics that do not contain PBDE but contain other brominated flame retardants are also reported to contain bromine.
How often should we retest if all screening passes?
Depending on risk level and supply stability. With high-risk materials, testing should be performed periodically and immediately when there is a change in supplier or material formulation.
7. Conclusion
XRF and wet testing are two tools of the same strategy: screening for detection and control, analysis for conclusion and evidence. Mixing the roles of the two tools is a common cause of two types of mistakes: excessive testing costs, or overconfidence in screening results.
Three things to do: classify materials according to risk level; specify when a screening result must be converted to wet testing; and save both the screening results and test reports in the same file to see control history.
References
- IEC 62321 series — sections on screening and determination of restricted substances.
- Directive 2011/65/EU and its amendments (limits based on homogeneous materials).
- Guidance on the use of X-ray fluorescence in substance control is limited.
Related articles
- How is Cross Section different from X-ray, AOI and ultrasound? When must the sample be destroyed?
- RoHS and plastic recycling: why is it most difficult for recycled plastic to achieve RoHS?
- PVC and phthalates in cables: most common cause of limit exceedance
- Cr(VI) in the chromium passive layer: why does the mechanical and electronic industry often stick?
- XRF RoHS screening: how to read the results, how much to trust
- XRF reports “Cr” exceeds the limit: why is it not sure it is Cr(VI) and what should be tested next?
- Cr(VI) test: how are colorimetric and ion chromatography (IC) different?
- Checklist of 20 RoHS control points for electronics factories (input – production – output)
Discuss further
Disclaimer
This article is an interpretive content compiled by us; not legal advice. Enterprises need to compare relevant documents/standards verbatim before applying them to specific products.
See more: Copyright Policy & Disclaimer by ticforall.com.